Short answer: Choose batch when your part mix changes often, your components are large or heavy, or your tonnage is uneven. Choose continuous when one or two part families run day after day at steady, high volume. Batch wins on flexibility; continuous wins on cost per kilogram.
Batch furnaces
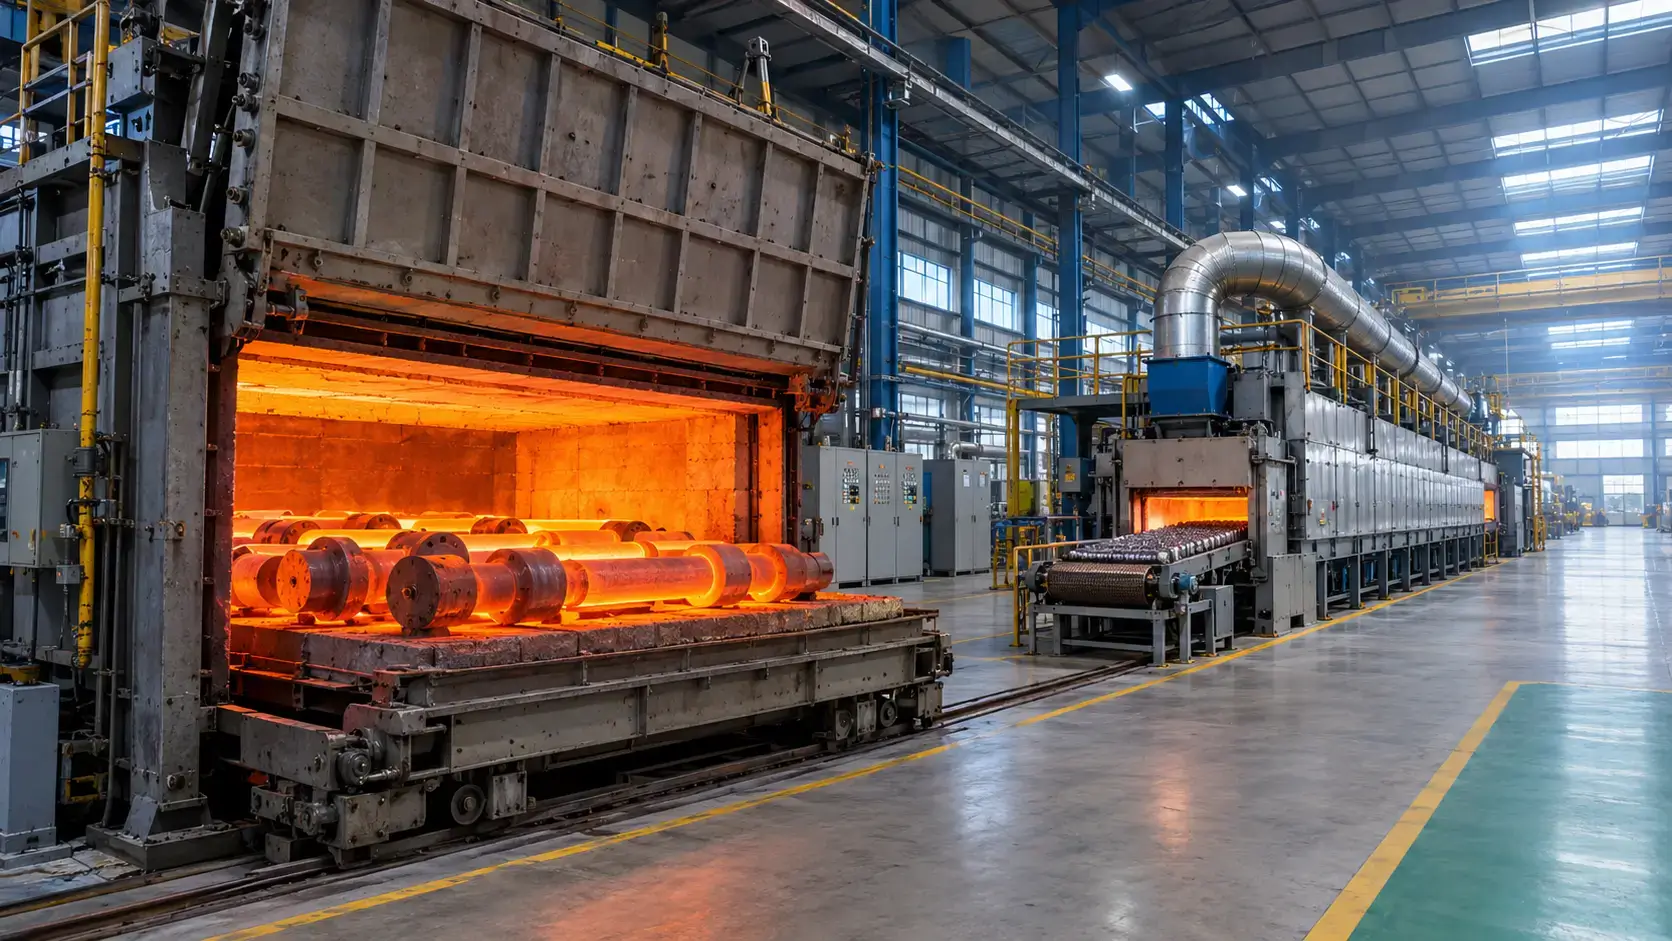
A batch furnace heats one charge at a time. The load goes in, the full cycle runs — ramp, soak, controlled cool — and the charge comes out before the next one enters. Every part sees the same cycle.
- Fixed hearth — the general-purpose workhorse for mixed job work.
- Bogie hearth — rail-mounted hearth that rolls out, for heavy forgings and large weldments.
- Box or bell — lift-off bell for coil annealing and bright annealing.
- Pit type — vertical chamber for shafts, tubes and long bars.
- Ladle preheater — ladle drying and refractory curing for foundries and melt shops.
Add a recirculation fan and uniformity tightens considerably — which is what tempering, ageing and solution treatment need.
Continuous furnaces
A continuous furnace keeps moving. Parts enter at one end, travel through fixed temperature zones and leave at the other, while the chamber holds temperature around the clock. Cycle time is set by conveyor speed and zone length.
- Pusher type — trays or skids pushed zone by zone; heavy charges, higher temperatures.
- Mesh belt — woven belt for fasteners, bearings and small stampings.
- Slat or conveyor — robust carriers for medium parts at steady throughput.
- Trolley type — preheat, soak and cooling zones for larger parts than a belt can take.
Because the chamber never cools, it avoids the biggest loss in batch work: reheating the structure and refractory on every cycle. See the full furnace range for capacities and temperatures.
The five criteria that decide it
1. Volume and steadiness
Steadiness matters more than peak tonnage. A continuous line is economical only when it runs loaded for long, uninterrupted stretches. At half capacity, or shut down every weekend, the saving disappears into holding losses and restart time. Swinging order books favour batch.
2. Part size
Continuous equipment has a fixed envelope, set at design stage. A 3-tonne forged shaft will not travel through a mesh belt line. Heavy, long or awkward components — typical heavy engineering work — need bogie hearth, pit or large fixed hearth furnaces.
3. Part mix
Count the distinct cycles you run in a month. A job-work heat treater with twenty customers and twenty recipes needs batch flexibility. A plant running the same gear blank daily pays for flexibility it never uses. Our heat treatment processes page maps each cycle to a furnace type.
4. Energy per kilogram
Batch furnaces reheat the furnace itself every cycle; continuous furnaces heat the structure once. At full sustained load that gives continuous a clear edge — but a line at 40 percent utilisation often costs more per kilogram than the batch furnaces it replaced. For Indian benchmark figures, see the Bureau of Energy Efficiency guidelines.
5. Uniformity and compliance
Both types hold tight uniformity, differently: batch proves one chamber with a temperature uniformity survey (TUS); continuous controls and surveys each zone. For SAE AMS2750 or AIAG CQI-9, both routes qualify — but both need documented TUS, SAT, calibrated instrumentation and traceable records. Specify that in the enquiry, not after commissioning. See our certifications and standards.
Capital cost and floor space follow from the above: continuous costs more up front and needs a long straight run; batch is compact and cheaper to install. Model payback on realistic utilisation over three years, not nameplate capacity.
Quick comparison
| Criterion | Batch | Continuous |
|---|---|---|
| Best suited to | Mixed, variable, low to medium volume | Steady, high volume, few part types |
| Part size | Large, heavy, long, awkward | Small to medium, uniform |
| Cycle flexibility | High — recipe per charge | Low — profile is fixed |
| Energy per kg | Higher | Lower at full load |
| Capital cost | Lower | Higher |
| Floor space | Compact | Long, linear |
| Labour per tonne | Higher | Lower |
| Idle penalty | Low — switch it off | High — holding losses |
Where each fits, by industry
| Industry | Usual answer |
|---|---|
| Forging | Batch — billet heating, normalizing, stress relieving; bogie hearth at the heavy end |
| Foundry and castings | Batch — annealing, normalizing, solutionizing, plus ladle preheaters |
| Automotive components | Both — continuous lines for volume parts, a batch furnace for development and rework |
| Aerospace and defence | Batch — small lots, full traceability, AMS2750 compliance |
| Railways | Batch — axles, couplers, springs and wheels on bogie hearth and pit furnaces |
| Aluminium and non-ferrous | Batch with recirculation — tight low-temperature uniformity for solution treatment and ageing |
| Steel and metal processing | Continuous where coil and strip volume justifies it |
Industry pages: forging, foundry, automotive, aerospace, railways, aluminium, steel, oil and gas.
Before you buy: modernise
A furnace with a sound shell and a tired control system is often a better investment than a replacement. Furnace modernisation — new burners, recuperation, ceramic fibre re-lining, PLC and SCADA control with audit-ready logging — cuts fuel consumption substantially at a fraction of new-furnace cost, and buys you the data to size a continuous line correctly.
What a manufacturer needs to quote
- Component description, maximum dimensions and unit weight
- Material grade or specification
- Process — hardening, annealing, normalizing, tempering, stress relieving, solutionizing, ageing
- Working temperature and required uniformity band
- Output in kg or pieces per hour, and shifts per day
- Fuel — electricity, natural gas, LPG, diesel or dual-fuel
- Applicable standard — AMS2750, CQI-9, ISO or customer QAP
- Floor space, bay height and crane capacity
Supply those eight and you get a comparable quotation. Leave them out and the price changes at the order stage.
Frequently asked questions
What is the difference between a batch furnace and a continuous furnace?
A batch furnace heats one charge at a time through a complete cycle before the next load enters. A continuous furnace keeps parts moving through fixed temperature zones while the chamber stays hot. Batch suits variable work; continuous suits steady, high-volume production of similar parts.
Which furnace is cheaper to run?
A continuous furnace gives lower energy cost per kilogram, because it heats the furnace structure once instead of on every cycle. That advantage only holds at sustained full load. Below roughly half utilisation, batch furnaces are usually cheaper to operate.
What production volume justifies a continuous furnace?
Steadiness matters more than peak tonnage. A continuous line makes sense when one or two part families run predictably across two or three shifts for most of the year. Irregular order books favour batch furnaces.
Can a continuous furnace handle large or heavy components?
Only within its fixed envelope, which is set at design stage. Heavy forgings, long shafts and large fabrications are normally handled by bogie hearth, pit or large fixed hearth batch furnaces. Pusher and trolley furnaces take heavier loads than mesh belt lines.
Do both furnace types meet AMS2750 and CQI-9?
Yes. Compliance depends on calibrated instrumentation, temperature uniformity surveys, system accuracy tests and a documented quality assurance plan — not on the furnace type itself.
Is it better to modernise an existing furnace or buy a new one?
If the shell and structure are sound, modernisation is usually the better value. New burners, recuperation, modern insulation and PLC or SCADA control can cut fuel consumption substantially at a fraction of new-furnace capital cost.
Talk to Mass Engrs
Mass Engrs Pvt Ltd builds and commissions batch and continuous heat treatment furnaces from two units at MIDC Kupwad, Sangli, with a sales office in Hyderabad — electric, gas, oil and dual-fuel, plus modernisation of existing furnaces.
Send the eight inputs above to sales@mass-engrs.com or contact our engineering team and we will come back with a recommendation and an indicative configuration. Phone 0233-2990599.
References
- SAE International, AMS2750G Pyrometry — aerospace pyrometry specification.
- AIAG, CQI-9 Special Process: Heat Treat System Assessment — automotive heat treat standard.
- Bureau of Energy Efficiency, Government of India, Energy Conservation Guidelines for Industries — process furnace benchmarks.
Hi, this is a comment.
To get started with moderating, editing, and deleting comments, please visit the Comments screen in the dashboard.
Commenter avatars come from Gravatar.