Short answer: AMS2750 governs how temperature is measured and proven. CQI-9 audits the whole heat treat operation, pyrometry included. Neither tells you which furnace to buy — but both decide the instrumentation, the number of control zones, the uniformity band and the documentation your supplier must deliver. Fix those at the enquiry stage, not at commissioning.
What AMS2750 requires
AMS2750 is SAE’s pyrometry specification, mandatory across aerospace heat treatment and the backbone of Nadcap heat treating accreditation. It covers five things: temperature sensors and their replacement intervals, instrumentation accuracy and calibration, correction factors and instrument offsets, system accuracy tests, and temperature uniformity surveys.
Two of those decide what the furnace must physically be:
- Furnace class — set by the uniformity tolerance your part specification demands. Tighter classes need more zones, better insulation, forced convection and more instrumentation. The class is not negotiable after purchase, so it must be in the enquiry.
- Instrumentation type — AMS2750 defines types A to E, A being the most heavily instrumented with load thermocouples and recording. Your customer’s specification names the type; the furnace is built to match it.
What CQI-9 requires
CQI-9, published by AIAG, is not a pyrometry spec — it is a self-assessment of the whole heat treat system, used across automotive supply chains. It covers management responsibility, floor and tooling control, process tables for each heat treat process, job audits and pyrometry, which it largely draws from the same principles as AMS2750.
For a furnace buyer, the practical consequences are the same: calibrated instrumentation, documented TUS and SAT at defined intervals, alarms on process-critical parameters, and recorded data you can show an auditor two years later.
AMS2750 vs CQI-9, side by side
| AMS2750 | CQI-9 | |
|---|---|---|
| Published by | SAE International | AIAG |
| Scope | Pyrometry only | The whole heat treat system |
| Used in | Aerospace and defence | Automotive supply chains |
| Enforced through | Nadcap audits and customer specs | Customer-mandated self-assessment |
| Covers furnace hardware | Indirectly, via class and instrumentation type | Indirectly, via process tables |
| Audit frequency | Per Nadcap or customer schedule | Typically annual self-assessment |
Plenty of Indian plants work to both — an aerospace and defence line next to an automotive components line. That is normal; the furnaces differ in class and instrumentation, not in principle.
TUS and SAT in one line each
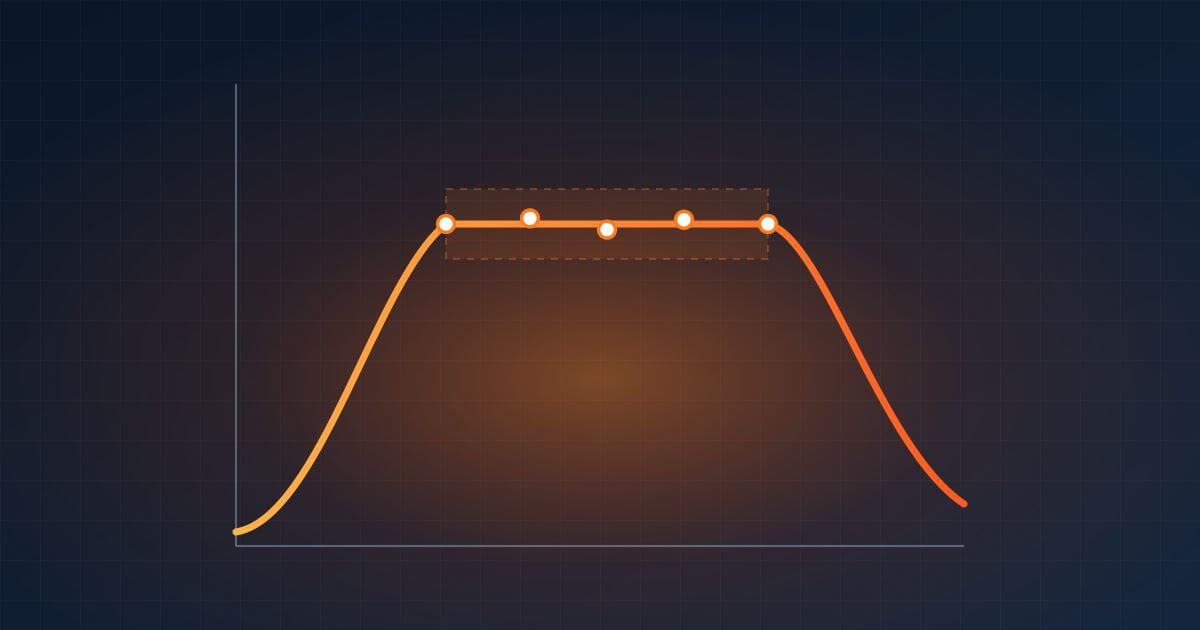
Temperature uniformity survey (TUS): thermocouples placed at defined positions across the working zone, proving the furnace holds the whole load inside the tolerance band of its class, at every qualified operating temperature.
System accuracy test (SAT): a calibrated test sensor placed beside the control thermocouple, proving that what the instrument reads matches the true temperature within the allowed limit.
Both are recurring, not one-off. A furnace passes at commissioning and must keep passing on schedule — which is why the test and documentation scope matters as much as the furnace itself.
Eight things to put in the enquiry
Send these with your RFQ and the quotations you get back will actually be comparable:
- Applicable standard and revision — AMS2750 (current revision), CQI-9, or a customer-specific QAP
- Required furnace class, stated as the uniformity tolerance from the part specification
- Required instrumentation type, and whether load thermocouples are needed
- Qualified operating temperature range, and the setpoints the TUS must cover
- Working zone dimensions — the TUS proves the working zone, not the chamber
- Recording and data retention requirement — paper, digital, retention period, audit access
- Who performs the initial TUS and SAT, and whether calibration certificates are traceable
- Alarm and interlock scope for over-temperature and sensor failure
The documentation pack to demand
A furnace that meets the standard but arrives without paperwork fails the audit anyway. Ask for all of this as part of the supply:
- Initial TUS report at every qualified setpoint, with thermocouple positions marked
- Initial SAT report
- Calibration certificates for every sensor and instrument, traceable to a national standard
- Instrument correction factors and offsets, documented
- Quality assurance plan (QAP) agreed before manufacture, not after
- Operating and maintenance manual including the TUS and SAT schedule
Does the furnace type matter?
Not for compliance. Batch and continuous furnaces both qualify — a batch furnace proves one chamber, a continuous furnace proves each zone. What changes is cost and effort: a multi-zone continuous line needs more survey positions and more instrumentation than a single-chamber bogie hearth or pit furnace. If you are still choosing between the two, read our batch vs continuous furnace guide first.
Upgrading an existing furnace
Compliance is often an instrumentation problem, not a furnace problem. If the shell and refractory are sound, furnace modernisation — new control and recording instrumentation, additional zones or recirculation, recalibrated sensors, a documented TUS and SAT schedule — brings an existing furnace into compliance for a fraction of replacement cost. Survey the furnace before you assume you need a new one.
Frequently asked questions
What is AMS2750?
AMS2750 is the SAE pyrometry specification used in aerospace heat treatment. It sets requirements for temperature sensors, instrumentation, calibration, correction factors, system accuracy tests and temperature uniformity surveys, so that parts are heat treated at the temperature the instruments report.
What is the difference between AMS2750 and CQI-9?
AMS2750 is a pyrometry specification: it governs how temperature is measured and proven. CQI-9 is a system assessment: it audits the whole heat treat operation, including pyrometry, process tables, management and job audits. Aerospace work uses AMS2750; automotive supply chains use CQI-9.
What is a temperature uniformity survey?
A TUS maps temperature across the working zone of a furnace using thermocouples at defined positions. It proves the furnace holds every part of the load within the tolerance band of its furnace class, at each qualified operating temperature.
What is a system accuracy test?
A SAT compares the furnace control or recording system against a calibrated test sensor placed next to the control thermocouple. It verifies that the reading the instrument shows matches the true temperature within the allowed limit.
Which furnace class do I need?
The class follows from the uniformity tolerance your part specification demands. Tighter classes require more heating zones, better insulation, forced convection and more control instrumentation, so they cost more. Fix the class from the part spec before asking for quotations.
Can an existing furnace be upgraded to meet AMS2750 or CQI-9?
Often yes. If the shell and refractory are sound, replacing control and recording instrumentation, adding zones or recirculation, recalibrating sensors and establishing a TUS and SAT schedule can bring an existing furnace into compliance at a fraction of replacement cost.
Talk to Mass Engrs
Mass Engrs Pvt Ltd builds batch and continuous heat treatment furnaces to AMS2750 and CQI-9 requirements, with documented TUS, SAT, calibrated instrumentation and an agreed QAP, from two units at MIDC Kupwad, Sangli. See our certifications and standards for what we supply documentation against.
Send your part specification and required furnace class to sales@mass-engrs.com or contact our engineering team. Phone: 0233-2990599
References
SAE International, AMS2750G Pyrometry — current revision of the aerospace pyrometry specification.
AIAG, CQI-9 Special Process: Heat Treat System Assessment — the automotive heat treat system assessment.
Performance Review Institute, Nadcap — the aerospace special-process accreditation programme.